The quote that came back 30 percent lighter
A distributor in Southeast Asia sent me two quotes last month for the same job: 60-metre rolls of 8.5 mil clear film, 1.52 m wide, both claiming aliphatic TPU and a ten-year warranty. One was 31 percent cheaper. He wanted to know which supplier was lying. Neither was: they were not selling the same film, and every difference sat in a layer no headline mentions.
Wholesale prices for unbranded and second-tier TPU PPF have fallen by roughly a quarter to a third since 2023. Some of that is genuine: more coating capacity, better yields. But a roll cannot shed 30 percent of its cost while every layer stays at full weight. Something got thinner or lighter, and if you don’t know which layer to weigh, you end up comparing boxes instead of protection.
Price is not a specification. Layers are.
A PPF build has four load-bearing numbers: topcoat, adhesive mass, caliper consistency, and liner. Marketing sheets describe the first in adjectives and skip the other three.
1. Topcoat thickness: 10 microns is a product, 6 is a different one
Real technical data sheets land the topcoat at 9.5 to 10.5 microns, premium lines at 12 to 15. Value-engineered rolls sit at 4 to 7 microns and call it “nano ceramic coating” without a micron figure. The gap between a clear TPU PPF line and its budget sibling from the same coating plant is often exactly this layer.
The topcoat carries stain release, hydrophobics, and the self-healing response, so a 6-micron coat has half the sacrificial material to give. Contact angle starts at 100 to 115 degrees and drifts below 85 within a year, which is where bird droppings start etching instead of rinsing. Useful heal cycles drop from five or six to two or three.
Ask for the layer table with methods: GB/T 7125 or ASTM D1003 for thickness, D7334 for contact angle.
2. Adhesive mass: 25 to 35 grams per square metre, or 18 to 22
Adhesive coat weight is the least glamorous number in the build and the one that decides whether an edge is still down in year two. Standard construction runs 25 to 35 g/m², giving 8 to 9 N/25 mm of initial peel and 12 to 18 N/25 mm at 24 hours — roughly 600 to 1,200 N/m in the ASTM D3330 geometry most buyers quote.
Cut it to 18 to 22 g/m² and nothing fails at delivery. At 12 to 18 months, bumper corners and wheel arch returns start lifting, because the adhesive has less mass to wet into the clearcoat and no reserve once heat cycling has done its work. Damp-heat retention exposes it: coupons at 65 °C and 90 percent RH for 72 hours should keep 70 to 80 percent of original peel. Rolls starting at 20 g/m² often retain 60 percent or less.
3. Caliper consistency, not just caliper
Everyone quotes total thickness; almost nobody quotes the tolerance around it. A 7.5 to 8.5 mil film sits at 180 to 215 microns, and normal commercial tolerance is plus or minus 5 percent. Value lines drift to 10 or 12 percent, so a roll labelled 200 microns can measure 178 at one end and 216 at the other.
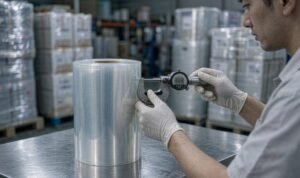
Take five readings per metre across three metres and calculate the coefficient of variation. Under 4 percent is a well-controlled line. At 7 percent you are buying thin lanes, and thin lanes haze first the moment an installer stretches a bumper. The same variance explains why two installers get different results from the same roll: one worked the thin lane, one didn’t.
4. Liner and release: where pre-stretch is born
The liner is a process control, not packaging. Standard builds use 75 to 85 micron PET with release at or below 0.3 N/25 mm and dimensional stability of 0.5 mm in machine direction, 0.4 mm across, over a 100 mm span.
Downgrade to a 50 micron or paper liner and two things change. Release force climbs, so the installer pulls harder to unroll and pre-stretches the film before it touches paint. And weaker dimensional stability keeps pulling the film’s own edges off the return. Neither shows up in a showroom inspection; both show up in the first summer. This is also where tiers hide: the real gap between TPH PPF film and TPU is base resin, but the gap inside a TPU range is usually topcoat and liner.
| What to ask for | Why it decides the outcome | Acceptable range |
|---|---|---|
| Topcoat thickness, with test method | Carries self-healing, stain release and UV load; first layer to be cut | 9 to 12 microns (premium 12 to 15); below 7 expect 2 to 3 heal cycles |
| Adhesive coat weight in g/m² | Sets initial grab and long-term edge hold | 25 to 35 g/m²; below 22 retention usually falls under 70 percent |
| Peel retained after damp heat | Predicts edge lift at 12 to 24 months, not at delivery | 70 to 80 percent or more of initial, D3330 with D4585 conditioning |
| Caliper variation across the roll | Thin lanes haze first when stretched | 180 to 215 microns total, plus or minus 5 percent; variation under 4 percent |
| Liner type and release force | Controls pre-stretch during unrolling | PET 75 to 85 microns, release at or below 0.3 N/25 mm |
| Colour shift after 300 hours, ASTM G154 | Separates aliphatic resin from blends | Delta b* of 2 or less, read per ASTM E313 |
| Price per square metre of usable film | Rolls differ in liner width and trim waste | Compare net of liner and 8 to 12 percent trim loss |
How to run the check in one afternoon
Step 1. Request the layer table, not the brochure: topcoat, TPU, adhesive in g/m², liner, and a method for each. Ranges that cover every competitor are not data.
Step 2. Measure caliper yourself, five points per metre, three metres apart, on the roll as delivered. A 20-dollar micrometer settles arguments.
Step 3. Cut 100 by 100 mm coupons, condition 72 hours at 65 °C and 90 percent RH, re-run peel. The most predictive test a buyer can run without a lab.
Step 4. Run 300 hours of ASTM G154 with an E313 colour read before and after. Delta b* under 2 passes; 3 and above looks tired on white paint inside three years.
Step 5. Install a bumper corner and a mirror cap, post-heat at 90 to 100 °C, leave 14 days, inspect edges under 1,000 to 1,500 lux raking light.
Step 6. Price per square metre of protection, net of liner and trim. This is where a 29 percent cheaper roll often becomes an 8 percent cheaper one.
What the numbers looked like on a real order
A 40-roll order, 1.52 by 15 metres, quoted at 6.40 USD per square metre from supplier A and 4.55 from B — 29 percent apart on paper. A measured 10.2 microns of topcoat, 152 microns of TPU, 29 g/m² of adhesive and 3.1 percent caliper variation. B came in at 6.1, 128, 21 and 8.4.
After conditioning, A retained 84 percent of its peel, B retained 61. After 300 hours of G154, A moved 0.8 on Delta b* against 2.9 for B, with haze rising 0.3 points versus 1.7. Fourteen months in the field across roughly 120 panels each, A had one lifted edge. B had seven at bumper corners and four hazy bonnets.
The direct money nearly cancelled out: about 1,690 USD saved on film, roughly 1,180 USD back in rework, plus four bonnets replaced under goodwill. On that batch the cheap roll was marginally ahead. What it cost was claim exposure across the remaining warranty years and one account that stopped reordering.
A cheap roll is not a scam. It is a specification you have not read
The 30 percent gap is information, not a warning label. Sometimes it buys a film that is genuinely adequate for a three-year lease return; sometimes it buys 128 microns of TPU under a six-micron coat that hazes before the second service. The only way to tell is to compare layers, mass and tolerance instead of claims. Buyers who ask for topcoat in microns, adhesive in grams and variation in percent get a different answer within one email. If you are still screening factories, pair this with a proper supplier audit before the first container, and start from a TPU PPF film source that publishes its layer table rather than its adjectives.