Three perfect rolls, one bad container
A distributor in the Midwest took a 380-roll container last spring. On the dock he opened three rolls, ran a micrometer over the liner side, held them to the light, and everything looked right. The paperwork matched, the driver was waiting. He signed.
Six weeks later, eleven of those rolls were peeling at 380 to 420 N/m on an ASTM D3330 pull test, against a purchase order that said 600 to 1,200. Four more measured 172 to 176 micrometres where the PO said 190 to 215. By then the film was on cars, and the argument was about who owned the labour. The supplier’s reply was two sentences: you inspected the goods, and you accepted them. That PO never said how many rolls had to be opened, or what counted as a defect. That is not a quality failure. It is a missing clause.
Why opening a few rolls proves nothing
The arithmetic is unforgiving. If one roll in twenty is defective, three clean draws pass 86 percent of the time. At an eight percent defect rate they still pass 78 percent. A buyer who opens three rolls, finds nothing and signs has learned almost nothing, but the signature survives.
AQL closes that gap. It stands for acceptance quality limit: the worst average defect level a buyer will tolerate across a series of lots, not a promise about the lot in front of you. ISO 2859-1 turns it into a sample size, an accept number and a reject number, so the decision stops being a conversation and becomes a count.
The four numbers that make a sampling clause work
1. The unit, roll or metre
A 1.52 by 15 metre roll carries 22.8 square metres, so a 380-roll lot is 8,664 metres. If the contract says “sample 200 units” and the unit is a metre, you have asked for nine rolls’ worth of film pulled from wherever the factory chooses, usually the head of the first roll. Set the unit as the roll and let the standard set the count.
2. The sample size
Under ISO 2859-1, general inspection level II, single sampling, normal inspection, lot size gives a code letter and that gives a sample: 20 rolls at 91 to 150, 32 at 151 to 280, 50 at 281 to 500, 80 at 501 to 1,200, 125 at 1,201 to 3,200. A 380-roll container lands on 50 rolls. At four minutes each that is three and a half hours, which is the entire cost of knowing.
3. The defect classes, written for film
Generic checklists fail here, because the defects that matter on film are not cosmetic. Split them three ways.
Critical, accepted at zero: wrong grade shipped, lot code absent from core or carton, unmarked splice, visible adhesive transfer on the liner, or a roll wound adhesive to adhesive. One of these fails the lot regardless of the count.
Major, at AQL 1.5: thickness outside plus or minus ten percent by ASTM D374, haze above two percent by ASTM D1003 against a 0.6 to 1.5 percent baseline, peel below 600 N/m by ASTM D3330 after 24 hours at 23 degrees and 50 percent relative humidity, width more than 3 mm off nominal, length short.
Minor, at AQL 4.0: liner wrinkles that do not print through, dented cores, label errors, edge wave under 2 mm.
4. The accept and reject numbers
At AQL 1.5 with a 50-roll sample, two defective rolls pass the lot and three fail it. At 80 rolls, three pass and four fail. Those numbers are not a target for the supplier and not a discount you are granting. They are the point at which the lot goes back, and they belong in the PO, because a rejection without a pre-agreed count is a negotiation.
| What to ask for | Why it matters | Acceptable range |
|---|---|---|
| Sample unit and sample size, quoted by lot size | Without a unit, any sample can be argued as compliant | Rolls as the unit; 50 rolls for 281 to 500, 80 for 501 to 1,200 |
| Defect list with critical, major and minor, each with an AQL | Turns poor quality into a countable decision | Critical zero, major 1.5, minor 4.0 |
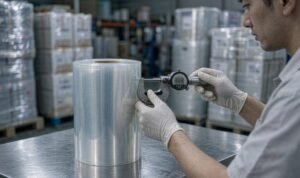
| Thickness at five points per sampled roll | A roll can average 200 micrometres and still run thin at the edge | 190 to 215 micrometres, plus or minus 10 percent, ASTM D374 |
| Haze and clarity on a 100 mm coupon | Haze is the defect buyers notice last and complain about first | 0.6 to 1.5 percent new, reject above 2 percent, ASTM D1003 |
| Peel at 24 hours, and after 72 hours at 65 degrees and 90 percent RH | Fresh peel describes the coating line, aged peel the adhesive | 600 to 1,200 N/m, retain 70 to 80 percent after ageing, ASTM D3330 and D4585 |
| Width, length and splice count per roll | Short rolls and hidden splices are the silent losses | 1,520 mm plus or minus 2 to 3 mm, length zero to plus 0.5 percent, one marked splice maximum |
The clause suppliers do not volunteer
ISO 2859-1 also carries switching rules, because it is built for a series of lots. Normal inspection tightens after two rejects in five consecutive lots, and can drop to reduced inspection after ten clean ones. Write both directions in. A supplier who accepts tightened inspection is telling you something about his process control; one who insists every container gets the same three-roll check has told you the check is decorative.
Running it in a warehouse, six steps
Step 1. Fix the unit, sample size, defect list and AQL in the PO before the deposit.
Step 2. Pull the sample at random across the container. Eight to twelve pallet positions, top, middle and bottom, suits a 40 foot load.
Step 3. Cut a 300 mm coupon from head, middle and tail of each sampled roll, labelled with the lot code. That catches drift along the winding.
Step 4. Measure in this order: thickness at five points, width with a steel rule, length by counting wraps, haze on a 100 mm square, peel last, because that test destroys the coupon.
Step 5. Score against the class list. One critical fails the lot. Two majors in fifty rolls pass, three reject.
Step 6. Log lot code, result and disposition on one sheet, and run the switching rules off it. Six months of records becomes a supplier ranking no sales deck can argue with.
What the inspection actually costs
A 380-roll programme at 8,664 square metres and 6.20 USD per square metre is about 53,700 USD of film, before freight. The dock check took forty minutes and missed eleven rolls at 380 to 420 N/m and four thin ones. The credit negotiation ran six weeks, replacement air freight came to 2,180 USD, and two installers lost nine days of bay time. Nobody could prove when the defect happened, so the supplier covered half.
In the sampled version, the same buyer spends 3.5 hours at 45 USD an hour, about 158 USD, plus 300 USD once for a micrometer and haze meter. On the next container, 50 rolls produced three majors against an accept number of two. That moved the lot to tightened inspection and a joint re-test, which found the coating line had drifted for two days. The lot was re-screened at the factory, and the buyer never saw the bad rolls.
The point is not the money saved on one container. It is that the reject number gave the buyer a reason to ask a process question, and the answer came back as a production record rather than a discount. Whether a supplier can produce that record is what our guide to vetting a PPF supplier before counterfeit film reaches your shop asks from another angle.
One clause, one number, one signature
Film is still sold on the assumption that buyers will judge it by feel, and most do, because nobody handed them a sample size. Any TPU PPF film programme big enough to fill a container justifies fifty rolls and three hours, and the same logic applies to clear TPU PPF bought on repeat, where the real risk is not a bad first lot but a slow drift nobody is counting. If a TPU PPF supplier will not put a sample size and an accept number in writing, he has already described what the last container looked like.