The bumper that came back in April
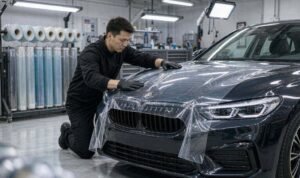
The job was a rear bumper on a dark grey estate, and it went out looking clean. The installer pulled one sheet over the reflector pocket, warmed it to about 70°C, pushed it in with a finger and a felt edge, and post-heated until it lay flat. Fourteen months later the customer sent a photo: the film had climbed back out of the pocket and stood 8 mm proud, with dirt packed into the gap behind it.
The shop replaced the section and called it a film problem. The pocket was 78 mm wide and 32 mm deep, which asks for roughly 26% stretch before the film touches the bottom, and that film had a comfort zone of about 10 to 15%. The installer got it in. The material then spent a year trying to get out.
It takes ninety seconds and almost nobody does it. Three numbers decide whether a recess goes in one piece, needs a relief cut or needs an inlay.
1. Measure the demand instead of eyeballing it
The demand is the extra length the recess needs, as a percentage of the flat distance across it. Tape gets you close: lay it across the widest part, press it into the deepest point, cut it there, and divide the gap by the original length.
Geometry is better and takes one line on a phone. Take half the channel width and the channel depth as the two short sides of a triangle, find the long side, double it, and compare with the original width. A 100 mm channel 30 mm deep needs about 17%. A 120 mm channel at 40 mm deep needs about 20%. Narrow it to 60 mm at the same 40 mm depth and the demand jumps to 67%. Depth alone is not the problem. Depth relative to width is.
Measure the worst pocket on the panel, not the average one. The worst one is the one that fails.
2. Know the usable budget, not the breaking point
Cast Car Wrap Vinyl stretches 30 to 40% before it tears, and that number is in every sales deck. Colour hold, gloss and adhesive integrity all live well below the breaking point.
The working budget for cast gloss is 10 to 15% where the colour has to stay true on a show face, and 20 to 25% is the absolute ceiling on a surface nobody inspects closely. Past 25% you are not stretching film, you are thinning pigment, and the panel reads lighter under a streetlight. Matte, metallic and colour-shift films are stricter, often 5 to 10%, because flake orientation and surface texture are the finish. A Color TPU PPF hits the same wall from the other side: the colour layer is thinner than a vinyl face film, so it goes pale at lower strain.
Calendered film is a different conversation: less stretch, more shrink-back, more memory. A recess that works in cast fails in calendered within a season.
3. Heat relaxes stress; it does not add stretch
The instinct when a pocket will not cooperate is more heat. That is the wrong lever. Heat lowers the force needed to reach a given strain, so the film goes in more easily, but the strain is still there when it cools. You have not reduced the demand, only hidden it until the first hot week.
Work the film at 40 to 60°C surface temperature and keep the adhesive line below 70 to 75°C. Above that you move adhesive rather than film and weaken the bond you paid for. The heat that matters comes last: post-heat every stretched area and edge to 88 to 95°C, roughly 10 to 15 seconds per 100 mm, which is what kills the film’s memory and sets the shape.
The shrink-back numbers explain why this is not optional. Cast film shrinks under 1% in service and calendered 2 to 4%. A pocket installed at 26% strain has a permanent reason to leave, and post-heating is the only thing that turns that energy into a set. Skip it and the film walks 6 to 10 mm out of the recess within a season, quietly, with the customer watching.
4. The seam geometry that decides whether the inlay holds
When demand exceeds budget you have two honest options and one dishonest one. Honest: a relief cut or an inlay. Dishonest: force it and hope the customer trades the car.
An inlay goes in first, into the deepest part of the recess, and the main sheet overlaps it by 8 to 12 mm. Put the seam where it cannot be seen: lowest point of the recess, or under trim that comes off anyway. Cut it with a straight edge and post-heat it before the main sheet goes near it, because a loose inlay edge lifts and takes the overlap with it.
A relief cut is cheaper and more visible. Cut from the deepest point outward, terminate in a small radius or a punched hole rather than a point, keep at least 10 mm from any panel edge, and overlap the flaps by 6 to 10 mm. A cut that ends in a point tears; a cut that ends in a radius stops. Seal every cut by overlap, never with a touch-up pen.
Either way, the seam is decided before the knife moves. Shops that decide after the film is tacked down finish with a starburst of relief cuts in a pocket that needed one.
The decision sheet
| What to check | Why it matters | Passing range |
|---|---|---|
| Required stretch, from tape or geometry | Tells you whether one piece is physically honest | Under 15% one piece; 15 to 25% single piece off the show face; above 25% cut or inlay |
| Working budget for that finish | Gloss, matte, metallic and colour layers differ | 10 to 15% cast gloss; 5 to 10% matte and colour-shift; 20 to 25% absolute ceiling |
| Film temperature during the pull | Heat hides strain, it does not remove it | 40 to 60°C surface; adhesive line below 70 to 75°C |
| Post-heat on every stretched area | Turns elastic memory into a set shape | 88 to 95°C, 10 to 15 seconds per 100 mm |
| Seam overlap and cut termination | Decides whether a seam holds or propagates | 8 to 12 mm overlap; cut ends in a radius, at least 10 mm from a panel edge |
Four steps and one shop’s numbers
Step 1. Measure the worst pocket before you unroll anything, and write the number on the job card next to the film name.
Step 2. Compare it with the film’s working budget, not its break elongation. Above 25%, plan the seam.
Step 3. If you cut, mark the line with fine tape, cut once, and terminate in a radius. Post-heat both flaps to 88 to 95°C before overlapping.
Step 4. Post-heat the whole recess after the overlap is squeegeed, then check it cold the next morning. A pocket that moved overnight was never set.
A shop in Leeds ran the same rear bumper on 22 cars. The first 9 went in one piece with heavy heat, and 7 came back with film proud of the pocket, averaging 2.5 hours to repair. The next 13 got a 40 mm inlay and one relief cut, about 22 minutes of extra labor each. None has lifted.
Seven repairs at 2.5 hours and 75 USD an hour is roughly 1,310 USD of unpaid labor, plus film and two customers who never came back. The inlay route added about 360 USD across 13 cars and produced no comebacks. The inlay looks expensive on the job card and behaves cheap in the accounts.
Where I land on this
Measure the recess, match it to a budget, then decide the seam before the knife touches film. A shop that can put a number on a pocket will beat one running on fifteen years of instinct, because instinct cannot be taught to a new installer and a number can. If your car film supplier cannot tell you the working stretch of the roll in your hand, fix that before you argue about price per metre.
The film almost never fails on its own. It fails where somebody asked it for 26% of something it had 15% of, then heated it until it looked like it worked. For the panel-level version of the same problem, this piece on where a wrap needs a seam covers the geometry no roll width can solve.