The splice that appeared in the middle of a roof
A wrap shop in the north of England takes a pallet of twenty rolls of gloss black cast. The van is blocking the yard at twenty to nine, the driver wants a signature, and the delivery note gets signed at the tailgate without anyone opening a carton. Standard morning.
Two weeks later an installer is laying a roof panel. Three metres into the roll there is a ridge under the film that will not squeegee flat — a splice, 120 mm of overlap bonded into the web, invisible until it is under a squeegee. The roof is cut again from a fresh roll, 4.4 metres gone, and a slot that was supposed to be a chrome delete moves to Thursday.
The supplier’s answer is that the splice was within specification. It probably was: one splice per 25 m roll is normal in this industry. The roll had also been accepted, in writing, at 8:40 that morning. Both statements are true, and the shop still paid for the roof.
Nothing on that pallet could be fixed at the install bay. Everything on it could have been caught in five minutes at the loading door, with a tape measure and a phone.
Four things a roll can hide
Width and the metres you actually get
A car wrap vinyl roll is sold at 1520 mm and 15, 18 or 25 metres. What you work with is usable square metres, and those are three different numbers once slitting tolerance, splices and trimmed ends are counted.
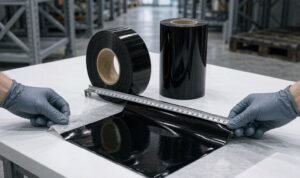
Twenty-five metres at 1520 mm is 38 m² gross. Take off two splice overlaps at 150 mm each, half a metre of damaged start and finish, and a width that measures 1517 mm, and you are at about 36 m² — five per cent gone before anyone touches a car. Standard tolerances are ±2-3 mm on width and minus zero to plus 0.5% on length. Measure both, at both ends and the middle, and write down what you measured.
Splices: count and position
A splice is not a defect. An unmarked splice in the wrong place is. Most film makers allow one per 25 m roll, and the convention is a flag on the outer wrap plus a marker tape on the liner so the installer can plan around it.
If you see no flag, unroll three metres and look. A splice ten centimetres from the end costs you a trim strip; the same splice three metres in costs a roof panel, and if it lands where two panels meet you may be re-cutting a door as well. It is the same planning problem as when a panel needs a seam, except this time you did not get to choose the line. The rule to put on the purchase order is short: maximum one splice per roll, flagged on the outside, none within two metres of either end.
Winding: telescope, edge crush, core
Telescoping is what happens when the layers slide sideways — the roll face looks like a staircase instead of a wall. More than 10 mm of stagger means the roll took heat in transit or was dropped on its side, and the edges beneath will be wavy. Wavy edges do not cut clean and do not lay flat along a door shut.
Edge crush shows as a corrugated rim. It is usually a strapping or pallet-stacking injury and it will cost you the first half metre of every wrap you cut from that roll. The core should be 76 mm internal diameter, centred, and undamaged. Stand the roll on a flat floor and let go: it should sit square, not lean.
Liner release and face condition
Peel 300 mm of liner back by hand at a steady speed. Resistance should be even — no snatching, no sudden releases, no adhesive transferring onto the liner. Blocking, where layers have bonded to each other in storage, shows as dull patches on a gloss face and as a tearing sound when you unroll.
Then look along the film at a raking angle in daylight. Gel spots, fisheyes and caliper banding all read as a faint orange-peel stripe once the film is on a panel, and none of them are fixable.
What to ask, and what counts as a pass
| What to ask | Why it matters | Acceptable range |
|---|---|---|
| Measured width at both ends and the middle | Sets usable area and whether edges will reach a recess | 1520 mm nominal, ±2-3 mm |
| Measured length against the label | Short rolls are the most common quiet loss | Minus 0% to plus 0.5% of nominal |
| Splice count and flagging | Decides whether a panel is scrap before you cut it | Max 1 per roll, flagged, none within 2 m of either end |
| Roll face stagger and edge condition | Predicts wavy edges, chatter cuts and lift | Stagger under 10 mm, no crush, no corrugation |
| Core diameter and condition | Winding tension and unwind behaviour | 76 mm ID, centred, undamaged |
| Liner release consistency | Adhesive shear during application | Even pull, no snatching, no transfer (test to ASTM D3330 on a sample) |
| Face defects under raking light | Visible after installation, unfixable later | No gels, fisheyes or caliper banding |
| Production date and stated shelf life | Vinyl has a clock that runs in the warehouse | Typically 2-3 years at 15-25 °C, 40-60% RH |
How to run the check
Step 1 — Paper before cardboard. Match the label to the purchase order: colour code, finish, width, length, batch and production date. A roll that has already spent eighteen months in a distributor’s rack is a different product from the one you ordered, which is how wrap vinyl quietly ages before it reaches you.
Step 2 — Stand it up. Telescope, edge crush, core, and whether the roll sits square on the floor. Ten seconds per roll.
Step 3 — Measure the width. Both ends and the middle. Photograph the tape against the roll face; a photo with a date beats a description in an email.
Step 4 — Unroll three metres on a clean bench. Look for splice flags, liner behaviour and edge quality. Mark three metres on the floor with tape while you are there, and check the second and third metres match.
Step 5 — Weigh one roll. Net weight within 2% of the declared figure. A short roll that measured correctly will show up here, because film weight scales with area.
Step 6 — Cut a 300 mm sample and use it. Apply to a scrap panel, post-heat at 90-100 °C, then check after 24 hours for edge lift and for adhesive transfer on removal. This is the only test that tells you how the roll behaves on a car rather than on a table.
Step 7 — Sign with a condition. Anything that fails gets photographed, quarantined with a label, and noted on the delivery note as received subject to inspection. That sentence is the difference between a claim and a conversation.
Two pallets, one invoice
Same colour code, same nominal size, two suppliers, twenty rolls each.
Supplier A quoted €158 a roll: 25 m nominal, measured average 24.4 m, width 1517 mm, six rolls carrying unmarked splices. Usable area per roll works out at 35.8 m², which is €4.41 per usable square metre.
Supplier B quoted €178: 25.1 m measured, 1520 mm, no splices. That gives 37.4 m² per roll and €4.76 per usable square metre.
On paper A is eleven per cent cheaper per roll and seven per cent cheaper per square metre. Then the pallet does its work: one roof panel re-cut after a splice surfaced (4.4 m of film plus 3.5 hours of labour), and one roll written off because a crushed edge made it useless for anything but jambs. Total for A lands within ten euros of B, with two days of schedule lost and one installer working Saturday.
The cheap pallet and the expensive pallet finished in the same place. One of them cost a weekend.
The position
Quality cannot be inspected into a roll at the install bay; it can only be confirmed or refused at the door. Five minutes, a tape measure, a camera and one sentence on the delivery note will not make a bad supplier good, but they will stop a bad pallet from becoming your labour cost. Buy from a car film supplier who flags splices and prints a production date, and the five minutes get shorter every month.