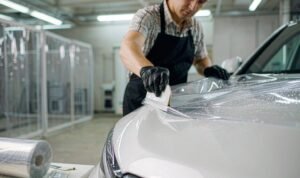
A distributor placed a 60-roll order last spring. The quote sheet read: TPU base film, 8 mil, self-healing clear coat, 10-year warranty. Every box was ticked. Fourteen months later, the front bumpers on a batch of white SUVs had turned the color of weak tea. The supplier’s answer was the sentence that should worry every installer reading this: “Our film is TPU, same as everyone’s.”
It is TPU. That is exactly the problem. “TPU” tells you the polymer family, not the grade, and it says nothing about whether the film survives 1,000 hours of desert UV. In 2026, with TPU holding roughly 85–90% of global PPF volume and PVC/TPE collapsing into the low-end corner, “TPU” has become a commodity label rather than a quality claim. The buying decision has moved down one level — into the chemistry nobody puts on the box.
This is a working guide to that level: what separates a film that stays clear for eight years from one that fails in eighteen months, how to test for it without a spectrometer, and what to write into a supplier agreement.
Why “TPU PPF” stopped meaning anything
Thermoplastic polyurethane is a block copolymer: hard segments (isocyanate plus chain extender) and soft segments (polyol). Change which isocyanate you use and you get two materials that behave identically on the install bay and diverge completely in sunlight.
Aromatic TPU is built on MDI or TDI. The aromatic ring is cheap, gives excellent tensile strength, and absorbs strongly in the 280–400 nm band — precisely where sunlight does its damage. Absorbed energy drives photo-oxidation, the backbone scissions, and the resulting chromophores show up as yellowing. This is not a coating defect you can wash off. The film itself is changing color.
Aliphatic TPU is built on HDI or IPDI. No conjugated aromatic ring, so the primary UV absorption pathway is largely absent. It holds color dramatically better, and costs meaningfully more per kilogram of resin.
Both are legally “TPU PPF film.” A quote sheet that says only “TPU” is not a specification — it is a category. And because film performance is judged on a white car where any shift is visible, that difference is the difference between a clean warranty record and a repaint-adjacent claim.
The four specifications that predict year-five performance
1. The isocyanate backbone
Ask for the resin type in writing, not the marketing name. Suppliers who use aliphatic volunteer it immediately, because it is a selling point. Suppliers who dodge the question are usually running aromatic and adding UV absorbers to buy time — which works, up to a point, and then stops. If you inherit stock with no paperwork, our guide on how to identify genuine aliphatic TPU PPF covers the bench checks that separate the two.
Sanity check: aliphatic film typically commands a 20–40% premium at roll level. If a “premium, no-yellowing” film sits at the aromatic floor, the resin is aromatic or the stabilizer package is doing work it cannot sustain for a decade.
2. The stabilizer package and its loading level
Even aliphatic TPU needs protection: a hindered amine light stabilizer (HALS) plus a UV absorber. What matters is the loading in parts per hundred resin, not the presence of the words on the datasheet. Under-loaded HALS is the most common hidden cost reduction in this industry, because it is invisible for the first year and catastrophic in the fourth.
Ask for the QUV data: ASTM G154 or ISO 4892-3, 1,000 hours, on a white painted panel, reported as CIELAB ΔE and yellowness index per ASTM E313. A film worth reselling should still be under ΔE 2.0 at that point. Under 1.5 is what good aliphatic formulations do.
3. The self-healing top coat
The clear coat is where “self-healing” lives: usually a crosslinked polyurethane or acrylic with mobile chain segments that re-flow above roughly 40–60 °C. That is why a hot day closes light scratches and a cold garage does not. For the underlying mechanism, see our breakdown of how self-healing TPU technology works.
Two numbers matter more than the phrase “self-healing”:
- Top coat thickness, typically 8–15 µm for a functional coat. Thin coats heal once and then stay scratched.
- Crosslink density, which trades heal rate against chemical resistance. A coat tuned purely for fast healing at low temperature is soft and grabs contamination.
4. The adhesive and what it leaves behind
Pressure-sensitive acrylic adhesives differ in initial tack, final bond strength, and — the one nobody tests until it is too late — residue on removal after five years of heat cycling. A high-tack adhesive that grabs instantly makes installation feel easy and makes removal a wet-sanding job. Look for controlled adhesion build, and specify residue-free removal in the contract.
| What to ask | Why it matters | Typical good value |
|---|---|---|
| Resin backbone | UV stability at the molecular level | Aliphatic (HDI/IPDI) |
| QUV 1,000 h, ΔE | Best predictor of visible yellowing | ΔE ≤ 2.0 |
| YI per ASTM E313 | Color shift on white paint | ≤ 3 after aging |
| Elongation at break | Conformability, impact absorption | 180–250% |
| Haze per ASTM D1003 | Optical clarity, orange-peel complaints | ≤ 1% |
| Top coat thickness | Healing durability | 8–15 µm |
| Adhesive removal | Labor cost at de-install | No residue, no paint lift |
Testing an incoming batch without a lab
You do not need a spectrophotometer to catch a substitution. You need a repeatable routine, run on every batch, with retained samples.
Step 1 — Documents before pallets. Require the technical datasheet, batch certificate of analysis, and a QUV aging report tied to the resin lot. If the COA is a photocopy with a handwritten batch number, treat it as marketing.
Step 2 — Control coupon. Cut a 100 × 100 mm sample from each roll, apply it to a white-painted steel panel the same way you would on a car, label it, and archive it. This is your evidence in a claim two years from now.
Step 3 — Accelerated UV check. Run coupons in a QUV chamber (UVA-340 lamps, condensation cycle) for 168–336 hours. This will not replicate five years, but aromatic resin shows measurable shift far earlier than aliphatic — the signal you want on a 72-hour turnaround. The same principle is what keeps 2026 TPU films clear on white paint: stabilization that survives the coupon test, not the datasheet.
Step 4 — Measure the shift. Below ΔE 1.0 is imperceptible. Around 2.0 a trained eye finds it on white. Above 3.0 the customer finds it. Compute it from L*a*b* readings:
"""CIELAB colour shift (CIE76) for PPF batch screening.
Pass/fail gates are deliberately conservative: they are meant to
catch resin substitution, not to certify five-year performance."""

def delta_e_76(lab_ref, lab_sample):
    l1, a1, b1 = lab_ref
    l2, a2, b2 = lab_sample
    return ((l2 - l1) ** 2 + (a2 - a1) ** 2 + (b2 - b1) ** 2) ** 0.5


def screen_roll(lab_before, lab_after_quv, hours=336):
    de = delta_e_76(lab_before, lab_after_quv)
    if de < 1.0:
        verdict = "PASS - imperceptible, consistent with aliphatic"
    elif de < 2.0:
        verdict = "WATCH - within tolerance, retain sample, retest at 1000 h"
    else:
        verdict = "FAIL - suspect aromatic substitution or under-loaded HALS"
    return {"hours": hours, "delta_e": round(de, 2), "verdict": verdict}


if __name__ == "__main__":
    white_panel = (95.2, -0.6, 0.9)
    after_336h = (94.6, -1.4, 4.1)
    print(screen_roll(white_panel, after_336h))
Step 5 — Mechanical sanity. Stretch a strip at low temperature. Aliphatic and aromatic films both stretch, but a film that snaps instead of yielding, or whitens at the fold, signals a blend rather than a designed TPU. Then peel a coupon off a scrap panel after 48 hours at 60 °C and inspect the paint for ghosting.
What a substitution actually costs
Back to that 60-roll order. We retrieved the archived coupons and ran 336 hours of QUV. Most of the batch sat at ΔE 1.1 — published-spec aliphatic, no argument. Four rolls came in at ΔE 3.8 with a visible straw cast, and their YI climbed from 1.9 to 6.4. Same product code, same packaging, same invoice. The supplier had filled the tail of the order from a second converting line running an aromatic blend.
The arithmetic is brutal in a way unit price never shows. Replacing four rolls is trivial. Replacing film on eleven delivered vehicles, plus telling a new Range Rover owner his hood has to be redone, is not. And the failure announces itself before the customer does — if you know what to look for, early-stage TPU PPF yellowing is visible on inspection long before a claim call.
The 2026 complication: layered protection and factory film
Two shifts are changing what “good film” means. The first is layering: PPF on impact zones, ceramic on top for gloss, hydrophobicity and chemical resistance. That works — if the coating is compatible with the top coat. A solvent-heavy ceramic applied before the adhesive has fully cured reliably produces edge lifting and a hazy finish. Respect the cure window, and never polish a self-healing coat with an aggressive compound.
The second is factory-installed film. OEMs increasingly offer PPF as a build option, which raises buyer expectations across the aftermarket and puts the pressure on documentation: batch traceability, electronic warranty registration, and a paper trail that survives a dealer change.
The checklist to put in your supplier agreement
- Resin type declared: aliphatic, with isocyanate class named.
- QUV 1,000 h ΔE and YI limits, with the test standard cited.
- HALS/UVA loading confirmed in the COA, not just the brochure.
- Top coat thickness range in µm, with a tolerance.
- Residue-free adhesive removal at end of service life.
- Batch traceability: every roll maps to a resin lot.
- Failed batch replaced at supplier cost, including labor.
Bottom line
The PPF market in 2026 is not short of film; it is short of verifiable film. Anyone can print “TPU” on a box, and most do. The operators who avoid the year-two yellowing call are the ones who stopped buying a category and started buying four specifications: backbone, stabilizer package, top coat, adhesive — each with a number attached and a test behind it.
Ask the question the quote sheet avoids. If the answer is a resin name and a ΔE figure, you have a supplier. If it is “same as everyone’s,” you have a warranty claim with your logo on it.